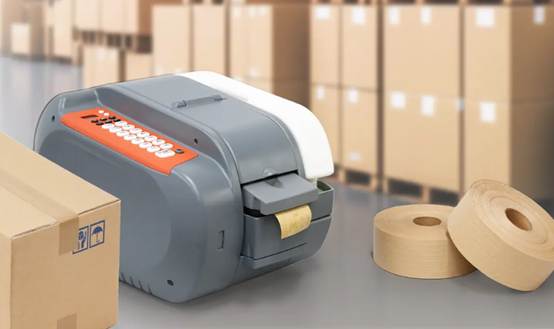
A carton sealed with water-activated kraft tape either bonds into the corrugated fibers or it does not. There is little middle ground, and the outcome is decided long before the carton reaches a carrier — it is decided at the moment the gummed paper tape dispenser moistens the adhesive. Too dry, and the tape lifts at the corners within hours. Too wet, and the starch turns soupy and the bond weakens. Even moisture across the full width is the variable that separates a dispenser that performs from one that produces rework.
Air Power Pak’s dispenser range covers four operating styles plus a measurement accessory. The useful way to read that range is not as a ladder from basic to advanced, but as four answers to different station realities.
The Handheld Option and Its Honest Limits
The GHC-50 is a manual handheld unit weighing roughly 330 g, with an 80 ml water reservoir, a moistening brush, and a cutting blade. It supports 50 mm tape width and roll diameters up to 140 mm, and is designed for standard non-reinforced kraft tape. No power connection, no installation.
Its value is portability: cartons can be sealed at the end of a packing table, beside a pallet being built, or on a cart moving between zones. Its limitation is equally clear. Output depends on operator technique. A steady pull gives the brush time to transfer moisture evenly; a fast, jerky pull leaves dry sections that never bond. Buyers evaluating this unit should test it on their own tape before committing, because the handheld format rewards rhythm and punishes haste.
The Lever Bench Unit: Standardization Without Electronics
The NT-800 supports tape widths from 20 to 100 mm, custom lengths up to 1000 mm, and roll diameters up to 200 mm. A single water fill covers roughly 100 to 200 standard cartons. The operator sets the length and pulls a lever; the machine feeds, moistens, and cuts.
This is the model most often misjudged during specification. Buyers sometimes order it expecting automatic length selection and discover the operator controls the length. For teams whose actual problem is inconsistent tape length across shifts, that manual control solves the problem directly — a set length is dispensed with every pull, so standardization happens without a circuit board. For high-throughput lines, it is the wrong tool, but that is a volume question rather than a quality one.
Where Automatic and Sensor Models Fit
The NT-AT 3.0 dispenses at 60 m/min, holds a 3.5 L water tank, and runs below 75 dB at shutoff. The larger tank reduces refill interruptions across a shift, and the delivery speed means a one-meter strip dispenses in about a second. For cross-border e-commerce operations processing high order volumes, those two figures compound across a working day.
The sensor-operated Tape-AT shifts the trigger to hand proximity, dispensing at an average of 60 m/min with a 2.5 L tank and adjustable water temperature from 0 to 80°C. The 45-degree case angle is set to reduce shoulder strain during extended use. This matters specifically where an operator holds a carton steady with one hand and cannot comfortably reach a button with the other — a routine situation at a standing packing bench. It adds less where cartons lie flat during sealing.
The Accessory That Addresses a Silent Cost
The UM-CJ01 tape length detector measures a carton placed near it and calculates the required tape length, with detection distance from 3 to 200 cm and accuracy within 1 cm. It works with the NT-ATv2.0 model. Manual estimation produces two failures that rarely surface in a cost report: tape cut short, requiring a second piece that compromises the seal, and tape cut long, wasting material on every carton. Across thousands of cartons, the second failure accumulates without anyone identifying the cause.
Five Confirmations Before Ordering
Tape width and roll diameter. Measure existing tape inventory before ordering equipment. A roll that does not fit the holder either goes unused or forces a return. This is the most common and most avoidable specification error.
Volume on the busiest shift. Count cartons per shift on the peak day, not the weekly average. An operation with a steady rhythm and a moderate count can reach consistent results with a lever bench unit; one sealing in the thousands per day will feel the manual pull before the shift ends.
Moistening consistency. Test a new unit on a dozen cartons and inspect the dried seals before scaling up. A dispenser that wets one edge more heavily than the other will produce corner lift-offs regardless of tank capacity.
Maintenance routine. Rinse the moistening brush weekly to clear dust and adhesive residue. Empty the reservoir before extended idle periods. Clear paper scraps from the blade area. These tasks take minutes and are the difference between years of service and a jam within a month.
Supplier support. For distributors and resellers, spare parts availability, warranty terms, and OEM/ODM flexibility — logo printing, body color, selected functions — determine whether the product line remains sustainable after the first order. Air Power Pak offers customization on selected models, with minimum order quantities and lead times that vary by model and project requirements. Sourcing dispensers and compatible kraft tape together simplifies matching, but tape specifications should be confirmed before bulk orders.
The Practical Conclusion
The right gummed paper tape dispenser is the one whose operating style matches how the station actually runs. Air Power Pak’s GHC-50 suits flexible, lower-volume packing; the NT-800 suits teams that want standardized lengths without electronics; the NT-AT 3.0 and Tape-AT suit repetitive, higher-volume sealing where reduced operator effort justifies added complexity. Start from carton count on the busiest shift, confirm tape width and roll diameter, and test seal quality on real cartons. Everything else follows from those three steps.